How to Conduct PPAP for Magnesium Alloy Die-Cast Components: APQP, Prototypes, and Submission Checklist
For automotive and high-volume procurement projects, this article outlines the documentation and evidence required—from APQP through PPAP—for magnesium alloy die-cast components, including drawings, process flow diagrams, PFMEA, control plans, MSA, capability studies, and material/performance test reports.
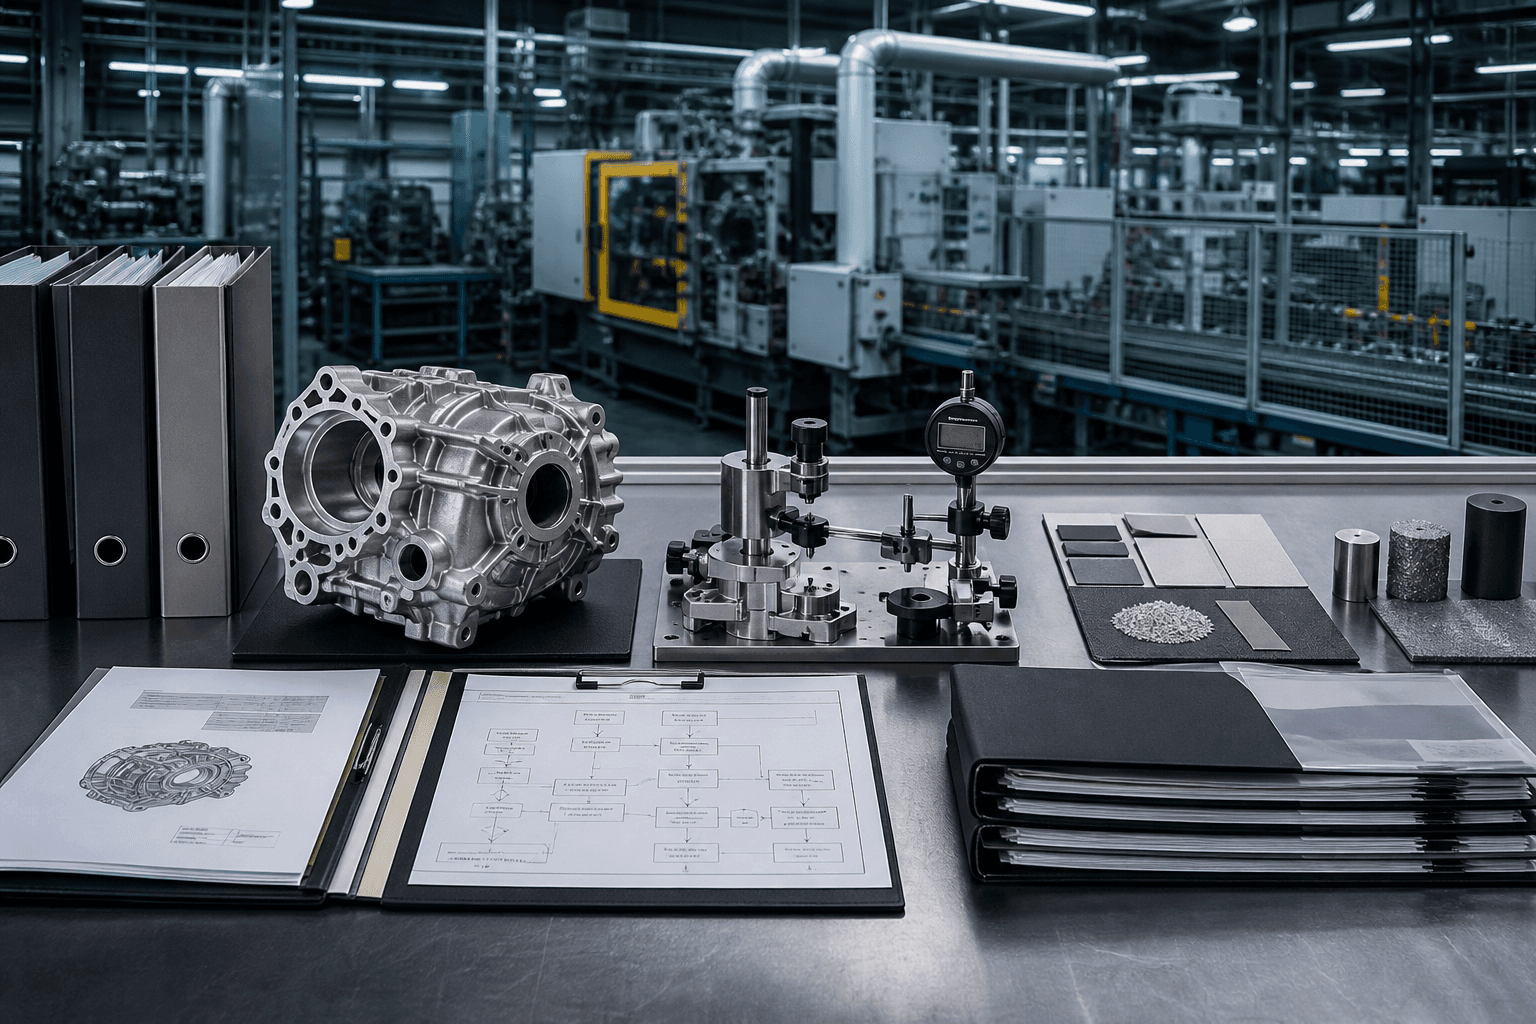
PPAP is not merely about completing a stack of templates—it is formal evidence that magnesium alloy die-cast components, produced using production-intent tooling, approved materials, qualified equipment, trained personnel, and specified cycle times, can consistently meet all requirements. APQP, meanwhile, must proactively translate material, mold, process, inspection, and supply-chain risks into an executable development plan.
Core Evidence Chain for Magnesium Die-Casting PPAP
| Document/Activity | What It Must Demonstrate |
|---|---|
| Design Record & Changes | Current drawings, specifications, and deviations are fully aligned |
| Process Flow Diagram | End-to-end coverage—from incoming material, melting, die-casting, to post-processing |
| PFMEA | High-risk failure modes, root causes, and prevention/detection actions are identified |
| Control Plan | Special characteristics, sampling frequency, measurement methods, and reaction plans are actionable |
| MSA | The measurement system can reliably distinguish true process variation |
| Initial Process Study | Key characteristics demonstrate capability under stable conditions |
| Material/Performance Reports | Composition, porosity, mechanical properties, leak-tightness, and coating performance meet requirements |
| PSW | Submission scope, level, and deviations are formally approved |
Common Oversights in Magnesium Alloy Projects
Molten metal protective gas and recycled material ratio are frequently omitted from process flow diagrams and PFMEA; vacuum curves, mold temperature, spray parameters, and die-casting settings are often stored only on machine HMIs—not linked to individual part traceability; reference CT/radiography images and measurement system capability are undefined; paint adhesion, corrosion resistance, and dissimilar-metal assembly validation—when delegated to Tier-2 suppliers—break the primary submission evidence chain.
Prototypes Must Be Produced Under Real Production Conditions
Prototypes selected manually, produced at low takt time, or inspected with temporary extra checks do not represent mass production. PPAP trial production must document material batch ID, recycled material ratio, cavity number, machine ID, mold revision, cycle time, unplanned downtime, parameter trend curves, and post-processing lot numbers. If customers approve temporary tooling or alternative processes, deviations and conditions for re-submission must be explicitly defined.
When Re-Submission or Notification Is Required
Tooling transfer/major overhaul, machine or furnace replacement, changes in raw material/recycled material source, protective gas or release agent substitution, significant adjustment of critical parameter windows, Tier-2 supplier changes, and resumption after extended shutdown—all may invalidate the original approval basis. Specific triggers follow customer requirements; internally, suppliers should maintain a more granular change review checklist.
Project Manager’s Checklist
- Are special characteristics consistently flowed down from drawings into PFMEA, control plans, and work instructions?
- Does every high-risk failure mode have both preventive and verifiable detection actions?
- Are capability data derived from a stable process—not mixed cavities or mixed shifts?
- Is the nonconformance reaction plan clear on quarantine scope and escalation path?
- Can sub-tier supplier certifications be traced to the final part batch?
- Do all deviations include expiration dates, responsible owners, and closure evidence?
Do Non-Automotive Customers Require PPAP?
A full automotive-style PPAP may not be mandatory—but its evidence-based framework applies broadly to high-volume projects and can be risk-adjusted into first-article approval, process approval, or a supplier quality package.
Need help preparing your magnesium die-casting PPAP or supplier submission package? Contact us via Contact Us with your customer tier and special characteristics; see available alloys in our Product Center.
Sources
https://www.aiag.org/docs/default-source/quality-/new-aiag-apqp-cp-what-you-need-to-know-to-be-ready.pdf AIAG PPAP, Fourth Edition