How to Use Die Release Agents for Magnesium Alloy Die Casting: A Troubleshooting Guide for Porosity, Carbon Buildup, and More
Covers die release agent concentration, spray coverage, atomization, mold temperature, drying time, and cycle timing to optimize demolding and cooling control in magnesium alloy die casting—enabling systematic troubleshooting of porosity, carbon buildup, sticking, and coating failures.
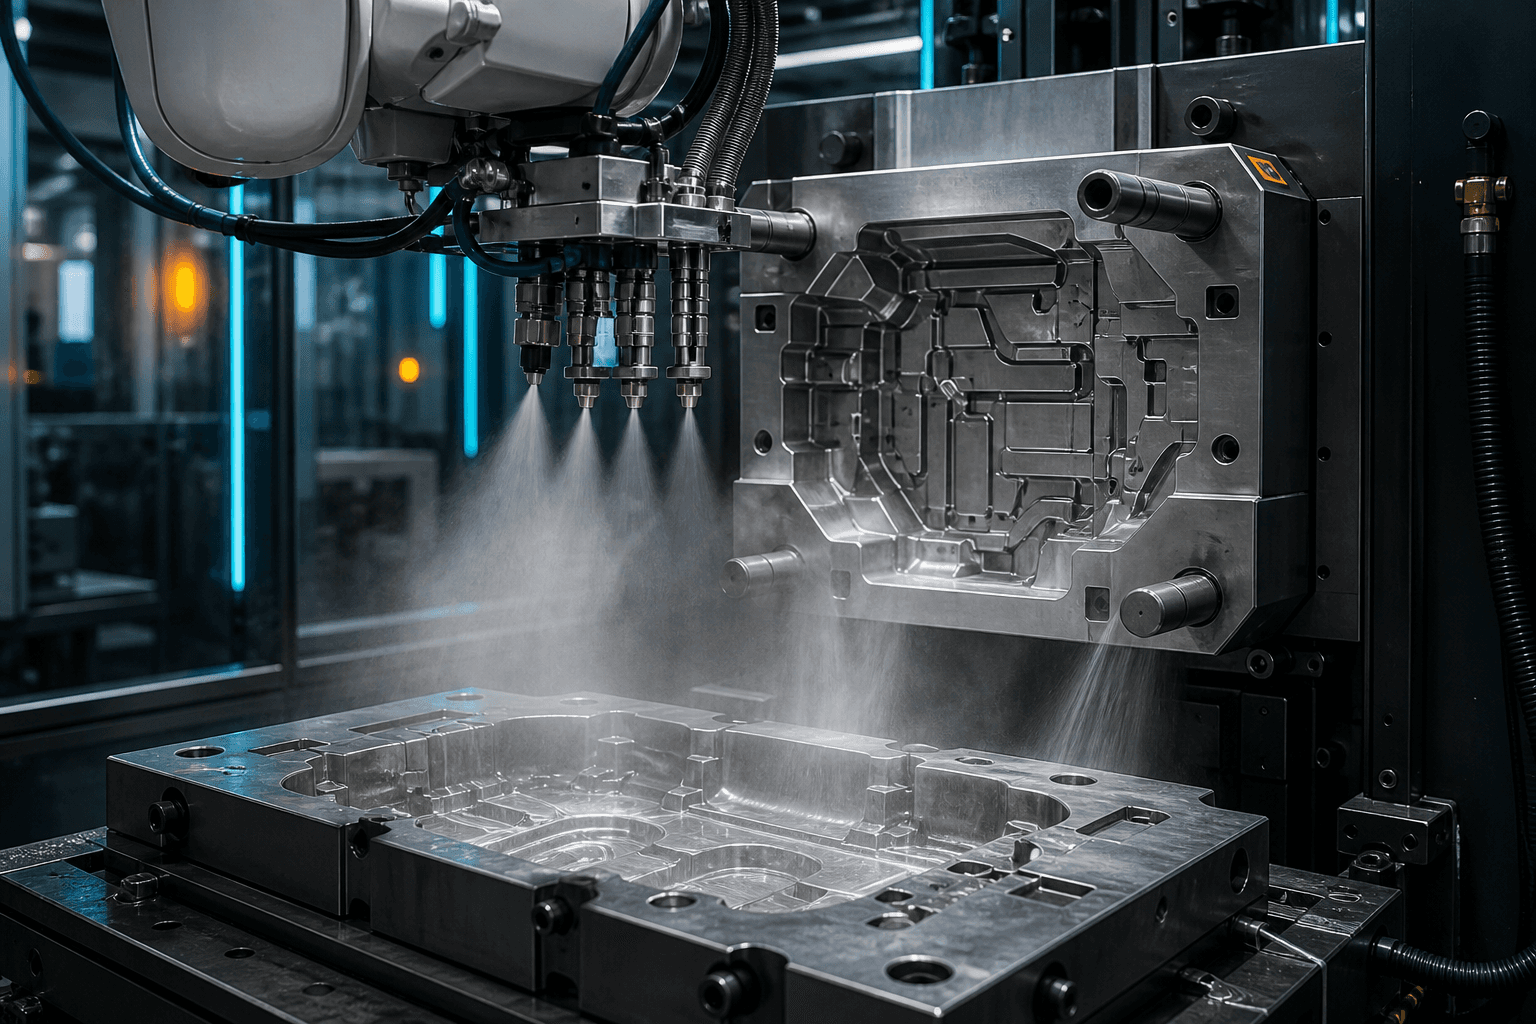
In magnesium alloy die casting, die release agents serve three critical functions simultaneously: demolding, localized lubrication, and mold cooling. However, the assumption that “more spray equals safer operation” often leads to porosity, carbon buildup, surface contamination, and subsequent coating failure. Stable production depends on controlled concentration, precise spray targeting, and thorough drying—not operator-driven touch-up sprays based on experience.
Four Critical Control Parameters
| Control Parameter | Common Issues When Out of Control |
|---|---|
| Dilution concentration / neat agent condition | Inadequate release, excessive residue, batch-to-batch variability |
| Spray volume and atomization quality | Oversized droplets, localized pooling, excessive cavity temperature drop |
| Spray location and timing | Incomplete coverage of critical zones; carbon buildup in non-essential areas |
| Air blow-off and evaporation time | Residual water or carrier entering the filling stage, causing gas entrapment and surface defects |
Why Porosity and Black Spots Occur
When droplets land on low-temperature cavities or deep recesses and fail to fully evaporate, the carrier may decompose during cavity filling—generating gas. Conversely, when temperatures are too high or spraying is chronically over-concentrated, solid components can carbonize and accumulate. Carbon buildup alters surface roughness, thermal conductivity, and vent cross-sections—leading to new issues including sticking, dimensional drift, and flow marks.
Making Spray Application a Reproducible Process
First, use thermal imaging to identify actual locations requiring cooling and lubrication. Then establish a repeatable program using fixed nozzles, distances, angles, pressures, flow rates, and durations. Solution preparation must include concentration verification via conductivity, refractometry, or supplier-recommended methods—and record water quality, solution temperature, and tank replenishment schedule. Deep cavities and slides must be verified for liquid pooling; air blow-off must fully cover all prone-to-residue areas.
Relationship with Downstream Processing
Die release agent residue can impair conversion coating, powder coating, painting, and adhesive bonding. A seemingly normal cleaning line does not guarantee complete contaminant removal. For high-adhesion or structural bonding applications, incorporate die release agent grade, maximum allowable spray dosage, and surface cleanliness into change management—and validate performance after humidity/thermal/corrosion aging tests.
Troubleshooting Sequence
- Freeze die release agent batch, concentration, nozzle program, and mold temperature;
- Inspect nozzle clogging, atomization quality, and robot trajectory;
- Observe cavity for pooling, carbon deposits, or localized overcooling;
- Correlate porosity/black spot locations with spray impact points;
- Adjust only one variable at a time—then verify demolding performance, porosity levels, and downstream process compatibility;
- Document the validated operational window in the process recipe and lock access permissions.
Can Die Release Agents Be Eliminated Entirely?
Certain processes allow substantial spray reduction—but feasibility depends on mold coating, alloy type (e.g., AZ31B, ZK61), part geometry, and ejection conditions. Any claim of elimination must be substantiated by continuous production data and measurable mold wear trends.
For assistance diagnosing porosity or coating issues linked to spray application, contact us at Contact Us with defect locations, mold temperature profiles, and spray programs. Product specifications are available in our Product Center.
Sources
NADCA Die Casting Defects — Causes and Solutions ASM Handbook, Volume 15 — Casting